
Service
Blow Molding
Cost-effective production of hollow plastic parts at volume using extrusion and injection blow molding.
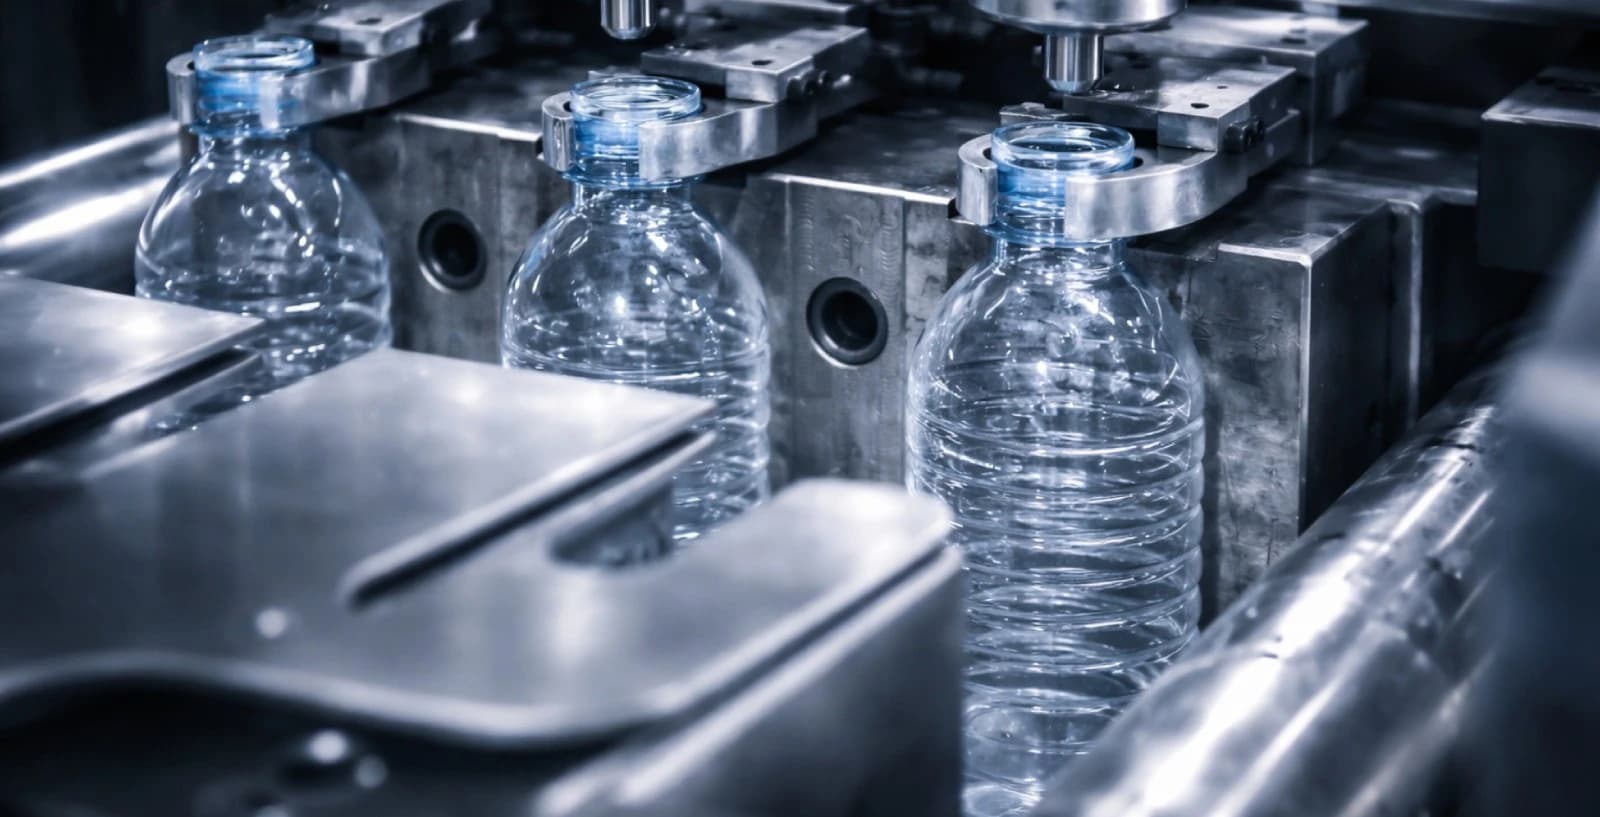
What's included
- {"text":"EBM for larger containers; IBM for precision neck finishes and tight dimensional control.","image":"https://nicerapidtooling.com/_next/image?url=%2Fimages%2Ficons%2Fblow-molding-feature-1.webp&w=3840&q=75","title":"Extrusion & injection blow"}
- {"text":"Co-extrusion with EVOH barrier layers for food, pharmaceutical, and chemical packaging.","image":"https://nicerapidtooling.com/_next/image?url=%2Fimages%2Ficons%2Fblow-molding-feature-2.webp&w=3840&q=75","title":"Multi-layer options"}
- {"text":"Blow moulds produced in 2–4 weeks for fast time-to-first-article and low tooling investment.","image":"https://nicerapidtooling.com/_next/image?url=%2Fimages%2Ficons%2Fblow-molding-feature-3.webp&w=3840&q=75","title":"Rapid aluminium tooling"}
- {"text":"Food-contact and pharmaceutical-grade materials available across all blow moulding processes.","image":"https://nicerapidtooling.com/_next/image?url=%2Fimages%2Ficons%2Fblow-molding-feature-4.webp&w=3840&q=75","title":"FDA-compliant materials"}
How it works
Part & Tool Design
Wall thickness, neck finish, and parting line designed. Aluminium blow mould CNC machined with cooling channels and pinch-off geometry.
Parison or Preform Production
EBM: molten parison extruded from die head. IBM: preform injection-moulded to precise weight and neck geometry.
Mould Close & Inflation
Mould halves close around parison. Compressed air (6–10 bar) inflated to expand plastic against mould wall.
Cooling
Mould cooling channels remove heat. Part solidifies in 10–60 seconds depending on wall thickness and material.
Demould & Flash Trim
Mould opens; part removed. Pinch-off flash at top and base removed by knife or automated trimming station.
Inspection & Labelling
Wall thickness gauge, drop test, and leak testing as required. Label application, cap assembly, and packing for dispatch.
About this service
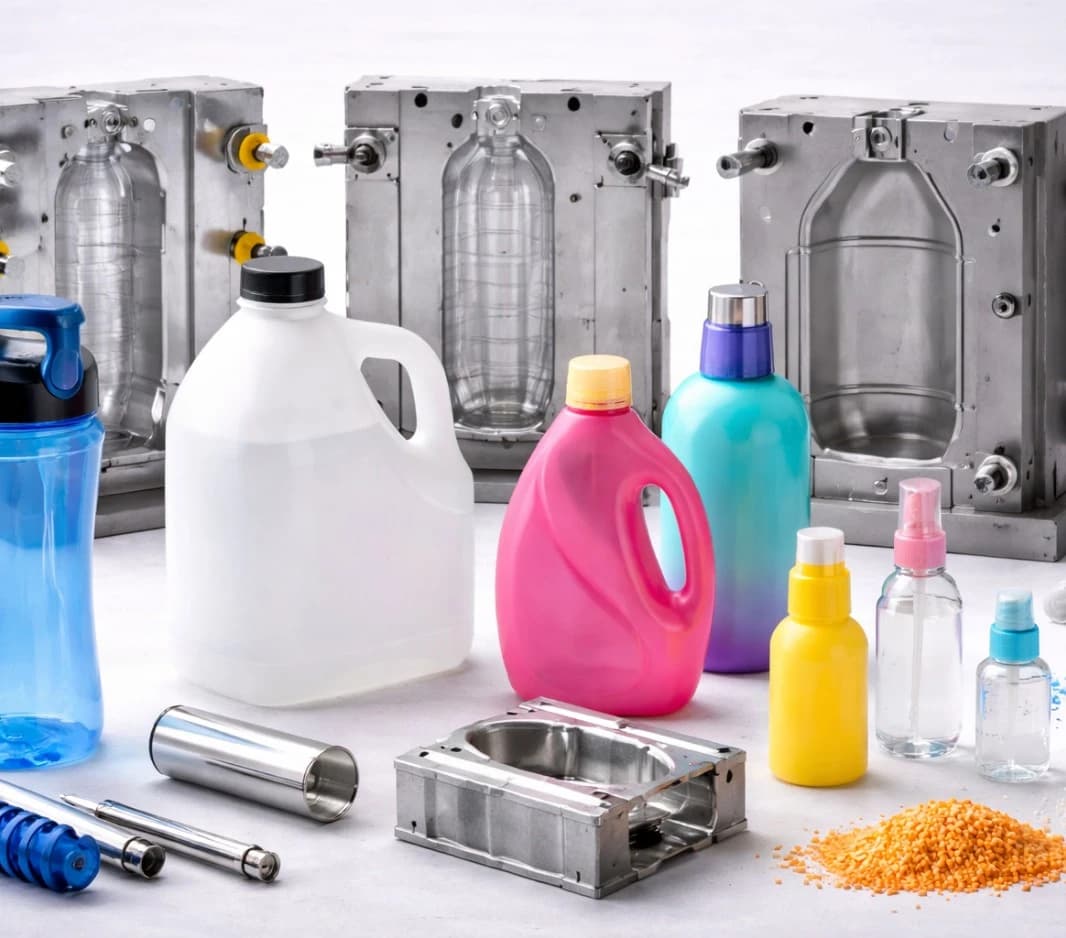
Blow moulding is the most cost-effective process for producing hollow plastic parts at volume. A parison or preform is inflated inside a closed mould to produce seamless hollow parts. Our tooling team designs aluminium moulds optimised for wall thickness control, material selection, and volume flexibility.
NICE Rapid operates extrusion and injection blow moulding equipment for hollow plastic parts. The right process and wall thickness are matched to your container geometry, material performance needs, and production volume.
What Sets Us Apart
- Extrusion & injection blow – EBM for larger containers; IBM for precision neck finishes and tight dimensional control.
- Multi-layer options – Co-extrusion with EVOH barrier layers for food, pharmaceutical, and chemical packaging.
- Rapid aluminium tooling – Blow moulds produced in 2–4 weeks for fast time-to-first-article and low tooling investment.
- FDA-compliant materials – Food-contact and pharmaceutical-grade materials available across all blow moulding processes.
Our Blow Moulding Capabilities
Extrusion Blow Moulding (EBM)
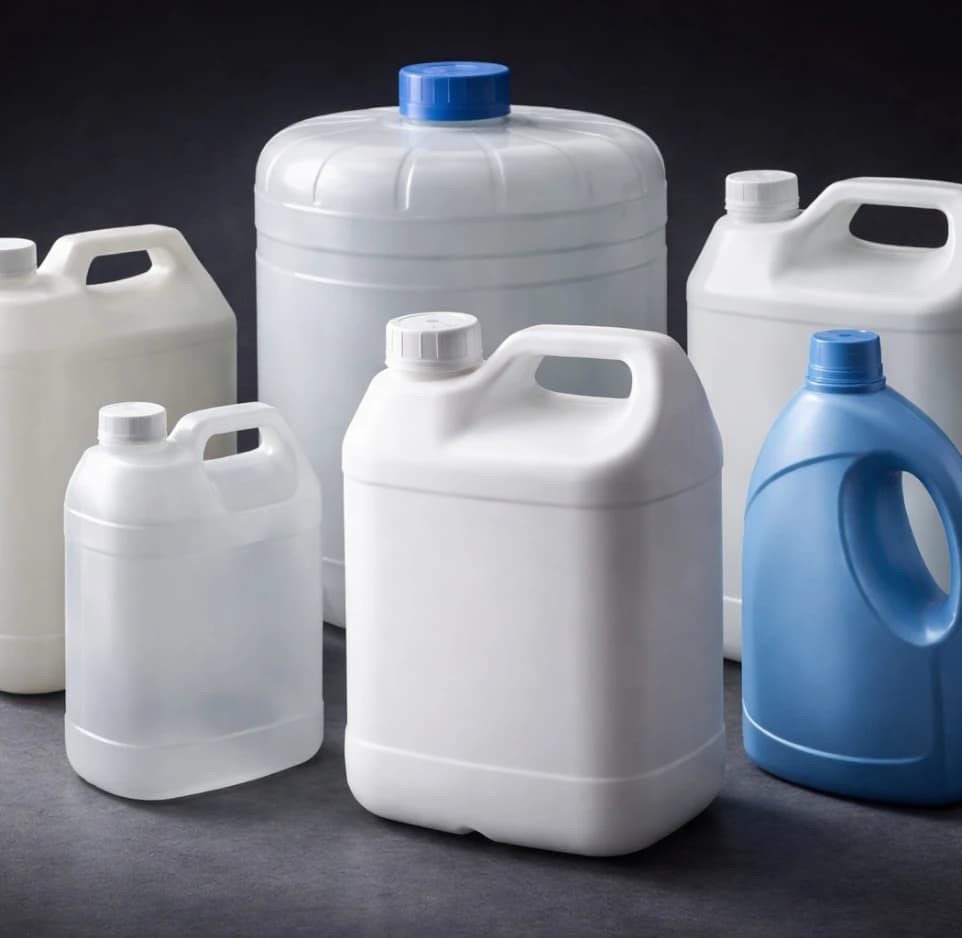
Molten parison extruded into open mould, mould closes and compressed air inflates part to mould shape. For bottles, containers, ducting, and non-round cross-sections.
Injection Blow Moulding (IBM)
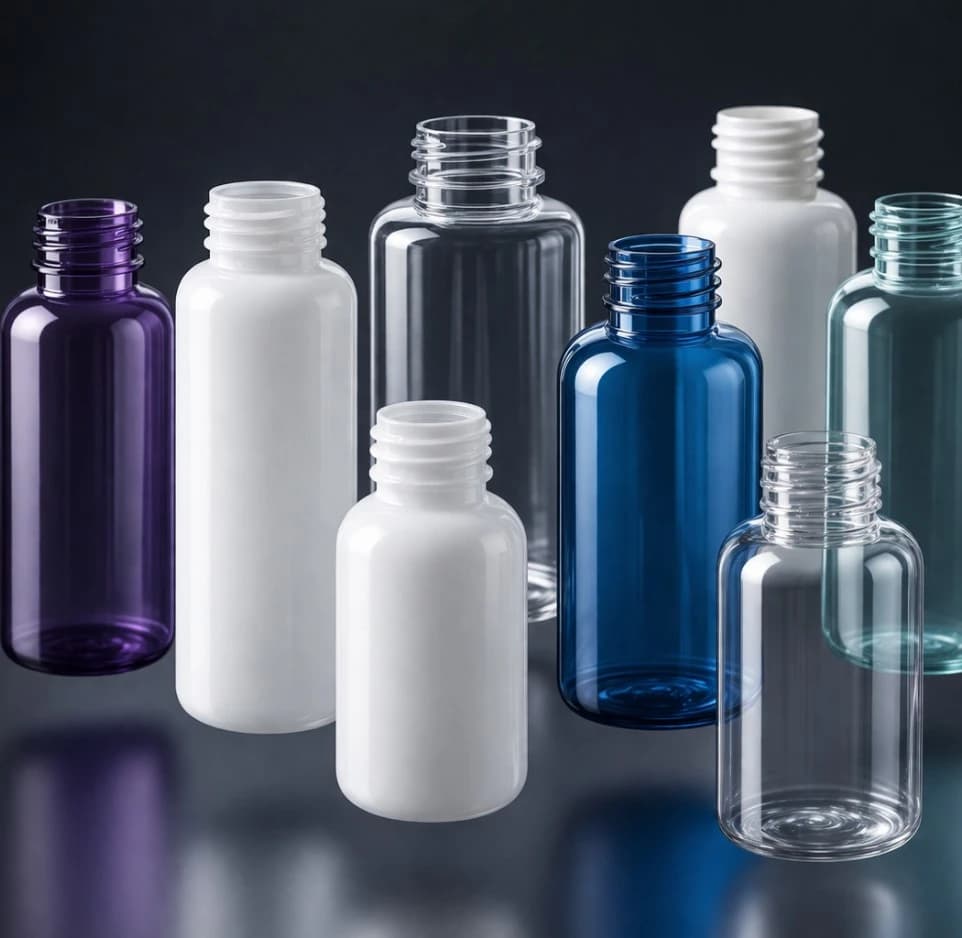
Preform injection moulded then blow-moulded for accurate neck finishes and tight dimensional control — ideal for pharmaceutical and precision packaging.
Multi-Layer Co-Extrusion
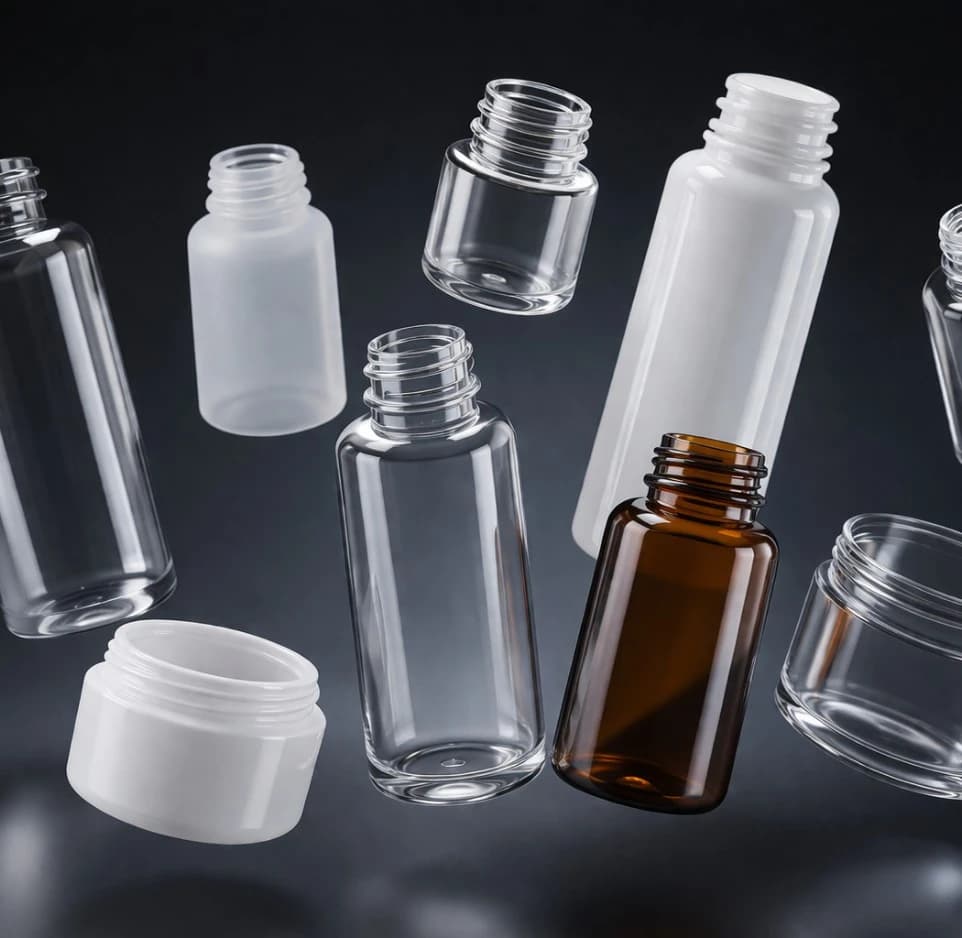
EVOH barrier layers co-extruded for food, pharmaceutical, and chemical packaging requiring extended shelf life and chemical resistance.
Our Process
- Part & Tool Design – Wall thickness, neck finish, and parting line designed. Aluminium blow mould CNC machined with cooling channels and pinch-off geometry.
- Parison or Preform Production – EBM: molten parison extruded from die head. IBM: preform injection-moulded to precise weight and neck geometry.
- Mould Close & Inflation – Mould halves close around parison. Compressed air (6–10 bar) inflated to expand plastic against mould wall.
- Cooling – Mould cooling channels remove heat. Part solidifies in 10–60 seconds depending on wall thickness and material.
- Demould & Flash Trim – Mould opens; part removed. Pinch-off flash at top and base removed by knife or automated trimming station.
- Inspection & Labelling – Wall thickness gauge, drop test, and leak testing as required. Label application, cap assembly, and packing for dispatch.
Materials
Polyolefins
| Material | Key Properties | Suitable Applications |
|---|---|---|
| HDPE | Chemical resistant, tough, recyclable | Bottles, drums, tanks, piping |
| LDPE | Flexible, soft, good clarity | Squeeze bottles, film liners |
| PP | Higher temp resistance, living hinges | Automotive reservoirs, food containers |
Transparent & Specialty
| Material | Key Properties | Suitable Applications |
|---|---|---|
| PET | Crystal clear, excellent barrier properties | Carbonated beverage bottles, food packaging |
| PETG | High clarity, easy to process | Cosmetic bottles, medical packaging |
| PC | Optical clarity, high impact | Headlamp lenses, protective containers |
| PVC | Flexible, chemical resistant | Medical tubing, industrial ducting |
| EVOH (co-extrusion) | Excellent barrier layer | Long shelf-life food and pharmaceutical packaging |
The Output
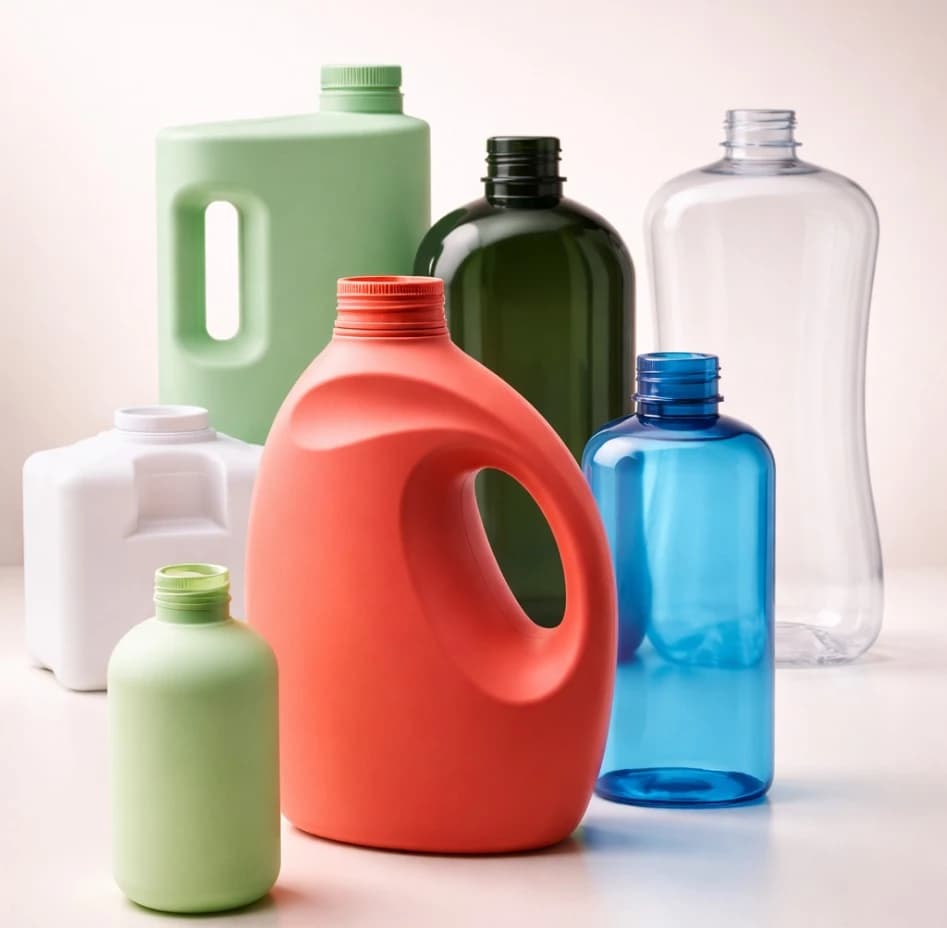
- Container volume: 50ml to 30L
- Wall thickness: 0.5mm to 4mm
- Neck finish: to DIN/ISO/custom specification
- Lead times: 2–4 weeks (tooling), then ongoing production
- Materials: HDPE, PP, PET, PETG, PVC, PC, EVOH multi-layer
- Available finishes: as-blown, labelled, printed, capped, assembled
Our Works
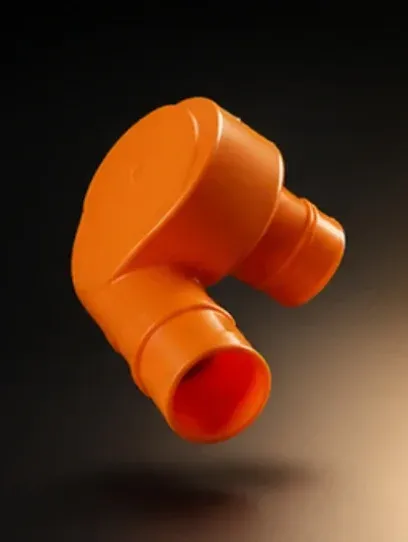
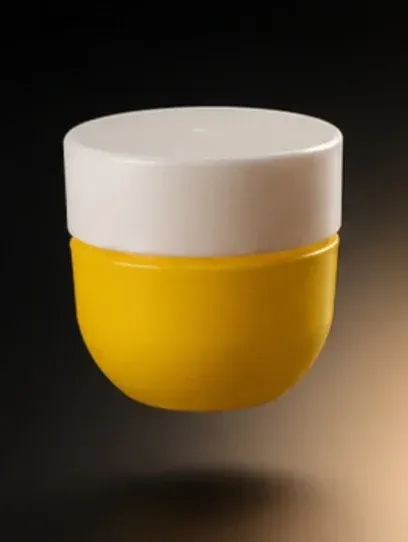
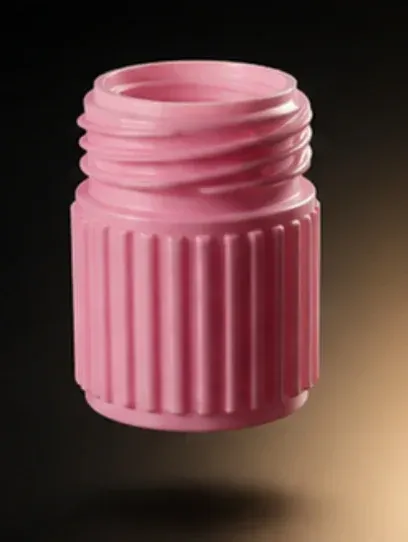
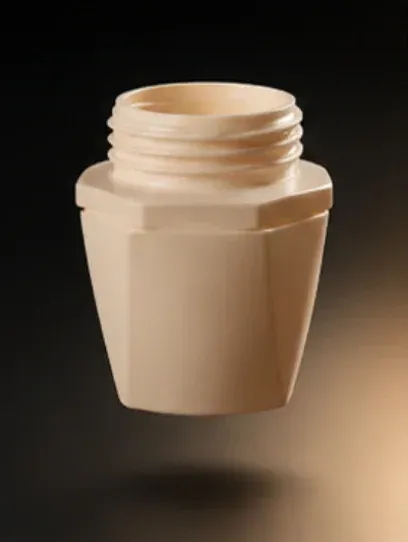
Industries We Serve
- Packaging
- Medical
- Automotive
- Consumer Products
- Industrial
Ready to Produce Your Container?
Upload your bottle or container design for a tooling review. Quote and lead time confirmed within 48 hours.