
Service
Pressure Die Casting
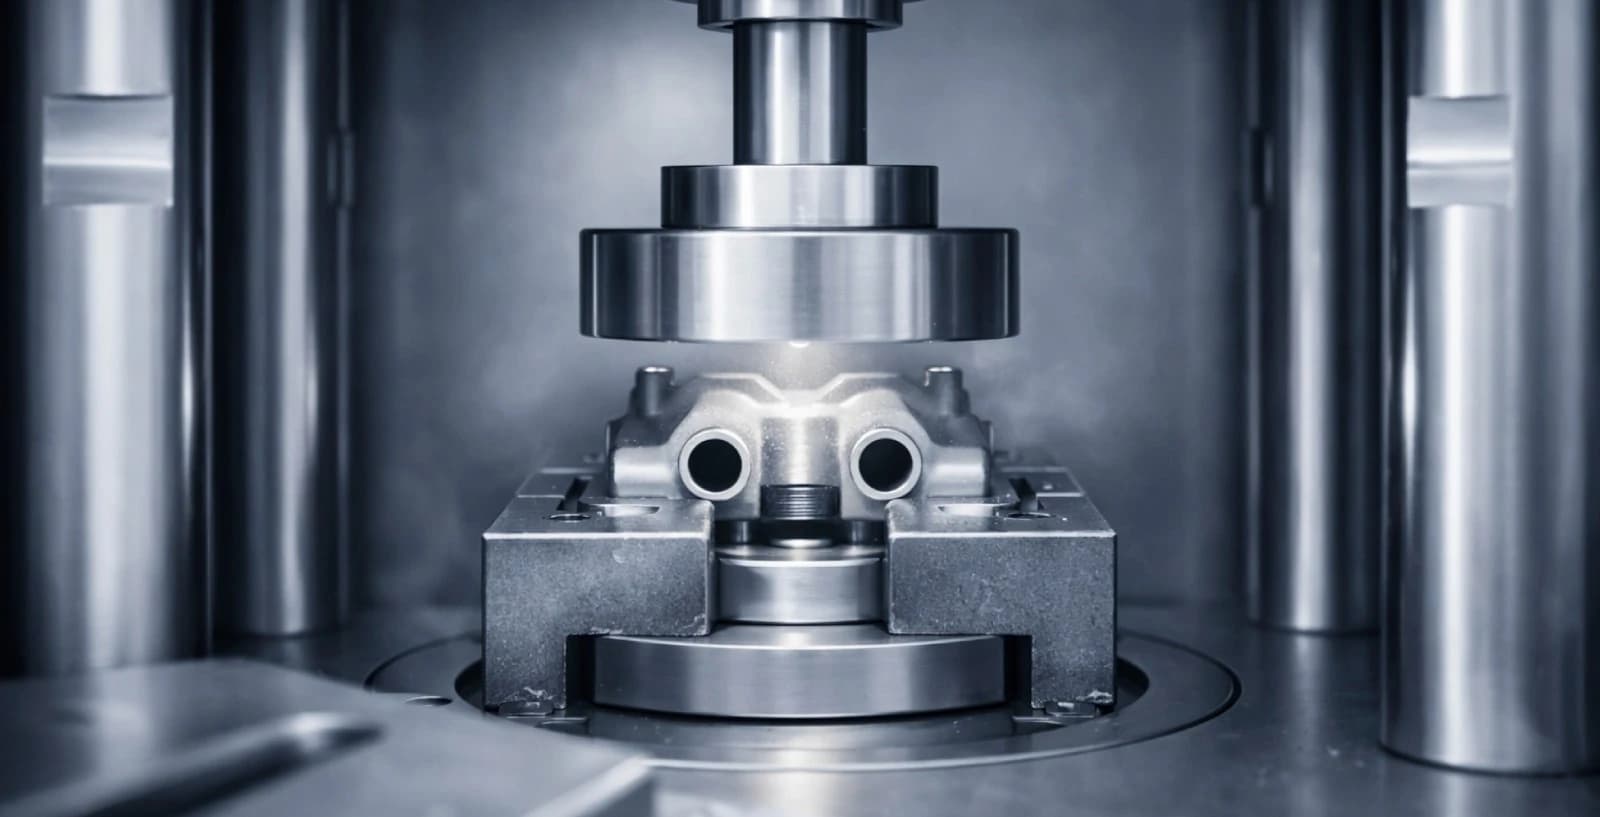
Pressure die casting injects molten metal into a hardened steel mold under high pressure to produce near-net-shape parts with tight tolerances and consistent surface quality.
What's included
- Cold chamber and hot chamber die casting in-house
- Tight tolerances
- Secondary operations
- ISO 9001:2015 certified
How it works
Die Design
Hardened steel die machined with cavity, runner, overflow, and cooling systems.
Die Trial
First production shots run to verify fill pattern, dimensions, and surface quality.
Process Optimisation
Shot pressure, injection speed, temperature, and cycle time optimised.
Volume Production
Parts produced at volume with in-process monitoring of key parameters.
Trimming and Cleaning
Flash trimmed, gates removed, parts shot blasted or vibratory finished.
Inspection and Dispatch
Dimensional inspection and pressure or leak testing where specified.
About this service
Pressure die casting injects molten metal into a hardened steel mold under high pressure. The metal solidifies rapidly to produce near-net-shape parts with tight tolerances and consistent surface quality. The process is suitable for high-volume production of complex metal parts in aluminium, zinc, and magnesium alloys. NICE Rapid operates both cold chamber (aluminium, copper) and hot chamber (zinc, magnesium) die casting at its Shenzhen facility.
What Sets Us Apart
- Cold chamber and hot chamber die casting in-house for aluminium, zinc, and magnesium alloys
- Tight tolerances of ±0.1mm on standard aluminium die castings
- CNC machining, surface treatment, and assembly managed in one facility
- ISO 9001:2015 certified with full inspection records per production batch
Our Die Casting Capabilities
Cold Chamber Die Casting — Used for metals with higher melting points, including aluminium and copper alloys. Molten metal is ladled into the shot chamber for each cycle. Suitable for structural brackets, engine housings, electronic enclosures, and heat-dissipating components.
Hot Chamber Die Casting — Used for zinc and magnesium alloys. The injection system remains submerged in the molten metal for faster cycle times. Suitable for small, precision zinc parts including connectors, locks, and decorative components.
Die Casting with CNC Post-Machining — Cast parts are CNC machined after casting to achieve tighter tolerances on critical features. Suitable for parts requiring both high volume and precision dimensions on mating surfaces.
Materials
| Material | Key Properties | Suitable Applications |
|---|---|---|
| Aluminium A380 | Most common Al alloy, excellent fluidity and castability | Automotive, electronics housings, structural brackets |
| Aluminium ADC12 | High silicon content, lower shrinkage | Thin-wall parts, complex geometry |
| Aluminium A360 | Better corrosion resistance than A380 | Marine, outdoor, food processing components |
| Zinc Zamak 3 | Good castability, high ductility | Small precision parts, connectors, decorative items |
| Zinc Zamak 5 | Higher strength than Zamak 3 | Mechanical parts, assemblies, hardware |
| Magnesium AZ91D | Lightest structural metal, good castability | Automotive panels, electronics housings |
| Copper Alloy (C83600) | High conductivity, corrosion resistant | Electrical components, marine, plumbing fittings |
The Output
- Typical tolerance: ±0.1-0.3mm; precision features to ±0.05mm with post-machining
- Surface roughness: Ra 0.8-3.2μm as-cast
- Minimum wall thickness: 0.8mm (aluminium); 0.5mm (zinc)
- Maximum casting weight: 25kg (cold chamber); 2kg (hot chamber)
- Lead time: 3-4 weeks (tooling); 5-10 days per production run after tooling approval
- Production volumes: 500-500,000+ parts per year
- Available finishes: as-cast, shot blasted, anodised, powder coated, painted, plated
Industries We Serve
- Automotive
- Consumer Electronics
- Telecommunications
- Industrial Equipment
- Lighting
Submit your CAD files for a die casting review. Tooling lead time and unit cost confirmed within 48 hours.