
Service
Liquid Silicone Rubber Molding
Precision liquid silicone rubber injection molding with in-house tooling, FDA and ISO 10993 certified materials, and tight tolerances to ±0.05–0.1mm.
What's included
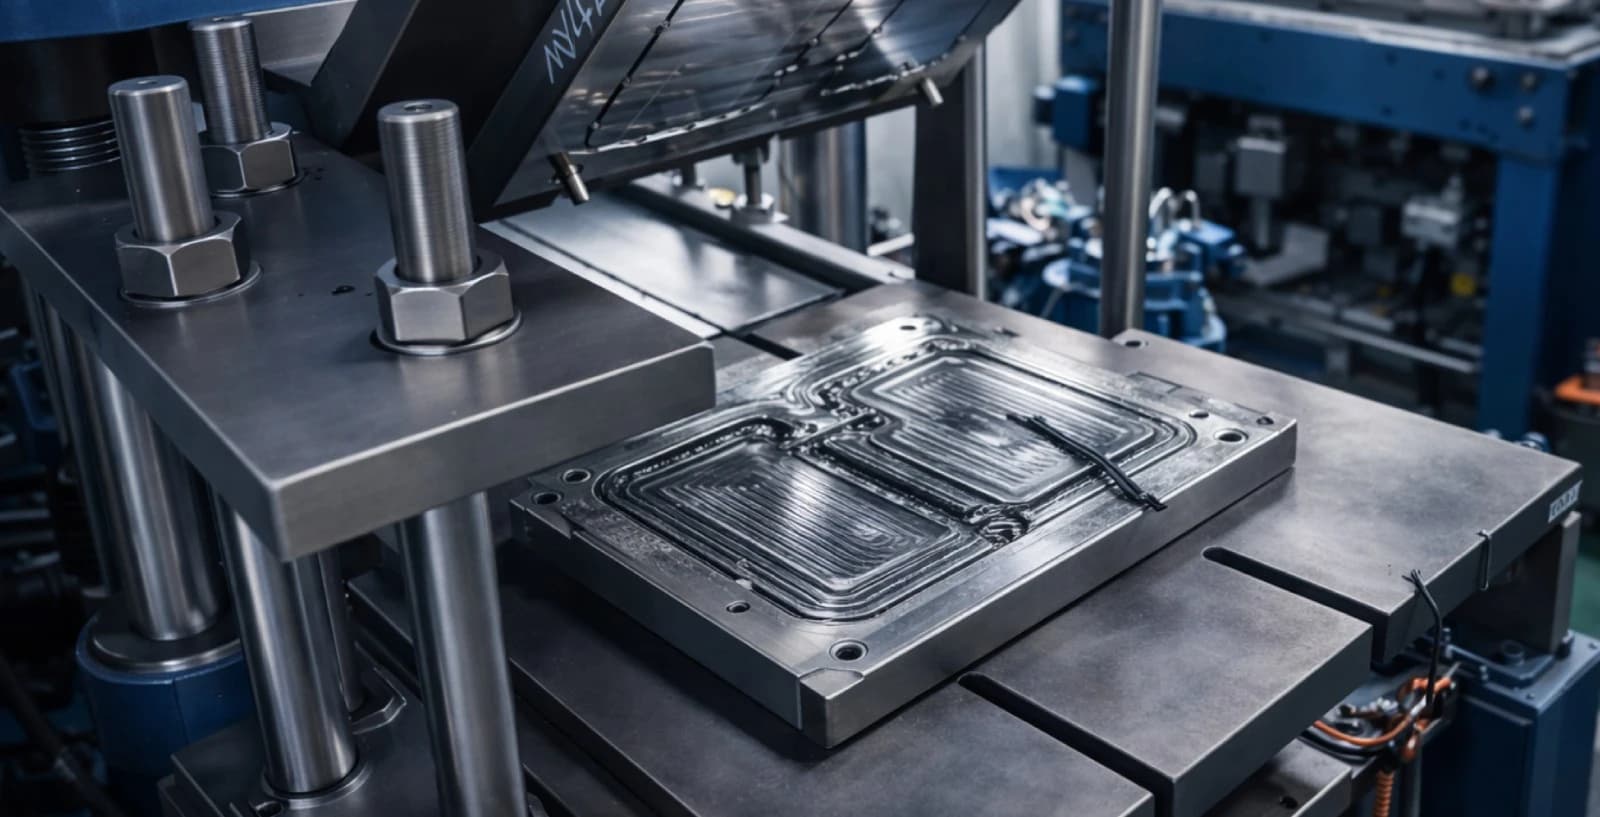
- {"text":"Self-sealing molds CNC machined at our Shenzhen facility. Tool builds and production runs under one roof — no subcontracting.","title":"LSR tooling built in-house"}
- {"text":"ISO 10993 and FDA 21 CFR certified grades available from standard inventory. No special order required for certified batches.","title":"Medical and food-grade compounds in stock"}
- {"text":"Consistent wall thickness across multi-cavity tooling. Automated metering maintains A/B mix ratio within ±1%.","title":"Tolerances to ±0.05–0.1mm"}
- {"text":"Medical-grade batches packed under controlled conditions. Certificate of conformance and full batch traceability records on request.","title":"Clean-room packing available"}
How it works
DFM Review
Wall thickness, parting line placement, gate location, and draft angles checked for LSR-specific flow behavior. Minimum wall thickness 0.4mm; undercuts and lifter requirements evaluated before tool design is confirmed.
Tooling
Self-sealing mold CNC machined from hardened steel. Cold runner system specified where material saving is required. First-article trial (T1) run and submitted for approval before production begins.
Compound Metering
A and B components metered at a precise 1:1 ratio via automated pump system. Color pigment or masterbatch added inline. Mix ratio maintained within ±1% throughout the production run.
Injection & Cure
Mixed compound injected at low pressure into mold heated to 150–200°C. Cure time ranges from 15 seconds to several minutes depending on wall thickness, mold temperature, and silicone grade.
Demolding & Post-Cure
Self-sealing tool geometry produces flash-free parts at ejection. Post-cure oven cycle (typically 4 hours at 200°C) removes residual volatile compounds — required for all medical and food-grade batches.
Inspection & Certification
Shore hardness, tensile strength, elongation, and critical dimensions inspected per batch. ISO 10993 and FDA certificate of conformance, full batch records, and clean-room packing available for regulated applications.
About this service
LSR molding injects a two-component liquid silicone compound into a closed, heated mold under pressure. The A and B components mix automatically at the injection unit, flow into the cavity, and cure in seconds to minutes at 150–200°C — producing dimensionally stable, flash-free parts with consistent wall thickness. The process is suited to complex silicone geometries that demand biocompatibility, chemical resistance, or a wide operating temperature range.
NICE Rapid runs dedicated LSR injection units with automated 2-component metering pumps and inline mixing systems. Tooling is CNC machined in-house with self-sealing cavity geometry — eliminating flash without secondary deflashing operations. From DFM review to first-article approval, most LSR tool builds complete in 3–5 weeks.
Capabilities
- LSR Injection Molding — Two-component liquid silicone metered, mixed inline, and injected into a self-sealing mold at 150–200°C. Produces flash-free parts with consistent geometry across multi-cavity tooling. Suitable for seals, diaphragms, valves, infant products, wearable components, and precision medical parts.
- LSR Overmolding — Liquid silicone injected directly over a thermoplastic substrate, forming a permanent bond without adhesives in a single shot. Suitable for soft-touch grips, sealed connectors, wearable patches, and medical device assemblies.
- Multi-Cavity & High-Volume Production — LSR tooling scaled from single-cavity prototype molds to 16-, 32-, or 64-cavity production tools. Automated demolding and pick-and-place systems support continuous high-volume runs.
Standard LSR Grades
- General-Purpose LSR — Wide shore hardness range, good long-term aging; industrial seals, gaskets, grommets, buttons.
- Food-Grade LSR (FDA 21 CFR) — Non-toxic, taste and odor neutral; kitchenware, baby products, food processing seals.
- Medical-Grade LSR (ISO 10993) — Biocompatible, sterilizable by autoclave, ETO, and gamma; implantable components, surgical instrument seals, drug delivery parts.
- High-Temperature LSR (to +230°C) — Thermally stable and UV resistant; under-hood seals, exhaust sensors, industrial high-temp applications.
Specialty LSR Grades
- Self-Lubricating LSR — Moving seals, check valves, catheter coatings.
- Electrically Conductive Silicone — Electronic gaskets, EMI shielding seals, keypads.
- Optically Clear Silicone — Lens covers, light guides, wearable optical components.
- Fluorosilicone (FVMQ) — Fuel system seals, aerospace O-rings, chemical plant gaskets.
Typical Output
- Shore hardness: A10 to A80 (LSR injection)
- Dimensional tolerance: ±0.05–0.1mm (LSR injection); tighter tolerances available on request
- Minimum wall thickness: 0.4mm (LSR injection)
- Temperature resistance: −60°C to +200°C standard; to +230°C (high-temp grades)
- Cavity counts: 1 to 64 cavities (volume dependent)
- Tooling lead time: 3–5 weeks (standard LSR tool build)
- Production lead time: 5–10 days after tooling approval
- Minimum order: no minimum
- Certifications available: FDA 21 CFR (food-grade), ISO 10993 (medical-grade), ISO 9001:2015
Industries Served
Medical and Life Sciences, Baby Products, Automotive, Consumer Electronics, Food Processing.